Carbon Fiber Machining Constraints for Structural Aerospace Parts
CFRP's weight savings vanish if machining constraints aren't engineered into design.
Carbon Fiber Machining Constraints for Structural Aerospace Parts.
Why CFRP has become structurally indispensable in aerospace despite the machining difficulty its strength numbers understate
Carbon fiber reinforced plastic earns its place on modern aircraft through a straightforward trade: high specific strength, high specific modulus, and resistance to corrosion and fatigue that aluminum and titanium simply can't match pound for pound ScienceDirect 2025 review. That's not a marginal improvement. On the Boeing 767, pushing CFRP content from 3% up to 50% of the airframe dropped fuselage mass from 60 tons to 48 tons, a documented case from a 2025 Elsevier review that shows what's at stake when composite content scales up ScienceDirect 2025 review.
Those numbers explain why CFRP now shows up in wings, tail fins, landing gear doors, and fuselage sections, all of them primary structural components that carry real load. But there's a catch buried in the material's own physics: composite structures can weigh in at 20% less than their metal equivalents, yet they're routinely harder to cut, drill, and trim into final shape. The weight win doesn't come free.
Five material properties don't act alone in causing that difficulty. Anisotropy, non-homogeneity, low interlaminar strength, a polymer matrix that's sensitive to heat, and fibers that are brittle rather than ductile all interact with each other during a cutting operation. Ignoring one property means the others don't compensate; they compound. This piece isn't here to relitigate whether CFRP belongs on a structural aircraft part. That decision's already made across the industry. What follows is a map of the constraints an engineer has to design around before geometry and tolerances get locked on a drawing. CFRP delivers a weight reduction of 30–50% and fuel savings of 20–25% versus aluminum and titanium alloys, according to the same review ScienceDirect 2025 review ScienceDirect 2025 review Industrial Monitor Direct.
Tool wear as the baseline economic and dimensional constraint
Start with the tool itself, because everything downstream traces back to it. A standard carbide cutter run against CFRP might last only a few feet of material before it loses dimensional stability, compared to 20 to 50 times that cutting distance in conventional metal work, according to a report from Mobility Engineering Technology. That phrase, dimensional stability failure, points to a tool that stops holding the tolerance the part needs well before its cost shows up on the cost line. A worn tool doesn't just need replacing sooner. It stops holding the tolerance the part needs, which means the feature it's cutting starts drifting out of spec in real time, mid-operation.
Polycrystalline diamond tooling changes that math substantially. PCD tools run 10 to 15 times longer than standard carbide, and diamond-veined tools, where diamond is sintered directly into the carbide body, open up cutting geometries that coated tools can't achieve at all. The reconditioning economics add another layer: resharpening a worn tool costs roughly 20% of buying new, and some PCD tooling can now be resharpened up to ten times before it's retired for good VizonFiber. That's a meaningful stretch on return per tool, and it changes how a shop plans tooling budgets across a production run.
None of this is just a procurement question, though. Part geometry drives how often a tool has to reposition and how long it stays engaged with material in one zone. Geometry that forces excessive repositioning, or that requires standard carbide in a tight-tolerance zone, will accelerate dimensional drift. Engineers laying out features need to think about tool engagement length the same way they think about wall thickness or hole spacing.
Multi-material stacks make the whole problem worse. CFRP paired with aluminum or titanium in a single stack-up means each material wants different cutting parameters, and titanium in particular can force a mid-cut parameter change partway through a single hole. A worn tool cutting through that kind of stack doesn't fail quietly. Tool wear causes delamination and surface damage immediately, which is exactly the next constraint on the list.
Delamination: how it forms during milling and drilling, and its effect on structural integrity
CFRP's interlaminar strength, the bond holding one ply to the next, is low compared to the strength within a single ply. Under cutting force, especially from a tool that's pushing rather than shearing cleanly, those layers start to separate. A dull tool makes this worse, because a dull edge pushes more than it cuts.
Research published in Multidiscipline Modeling in Materials and Structures in 2025 states that surface roughness and delamination during milling of CFRP aviation parts can lead straight to component rejection. Not rework. Rejection. That distinction matters on a structural aerospace part, where a delaminated zone near a load path isn't something you sand down and re-inspect. It's scrap.
Drilling carries the highest risk of any operation in this category. Through-hole drilling for rivets and fasteners is one of the most common secondary operations performed on structural CFRP, and it's precisely where cutting forces concentrate hardest, at the entry face and again at the exit face. Fuzzing, meaning uncut fibers left standing proud at the cut edge, appears alongside delamination and degrades the surface quality needed for bonding and assembly... Fuzzing is its own defect tied to fiber orientation and tool sharpness, distinct from how the material responds to heat, and it directly affects how well a joining surface will bond later.
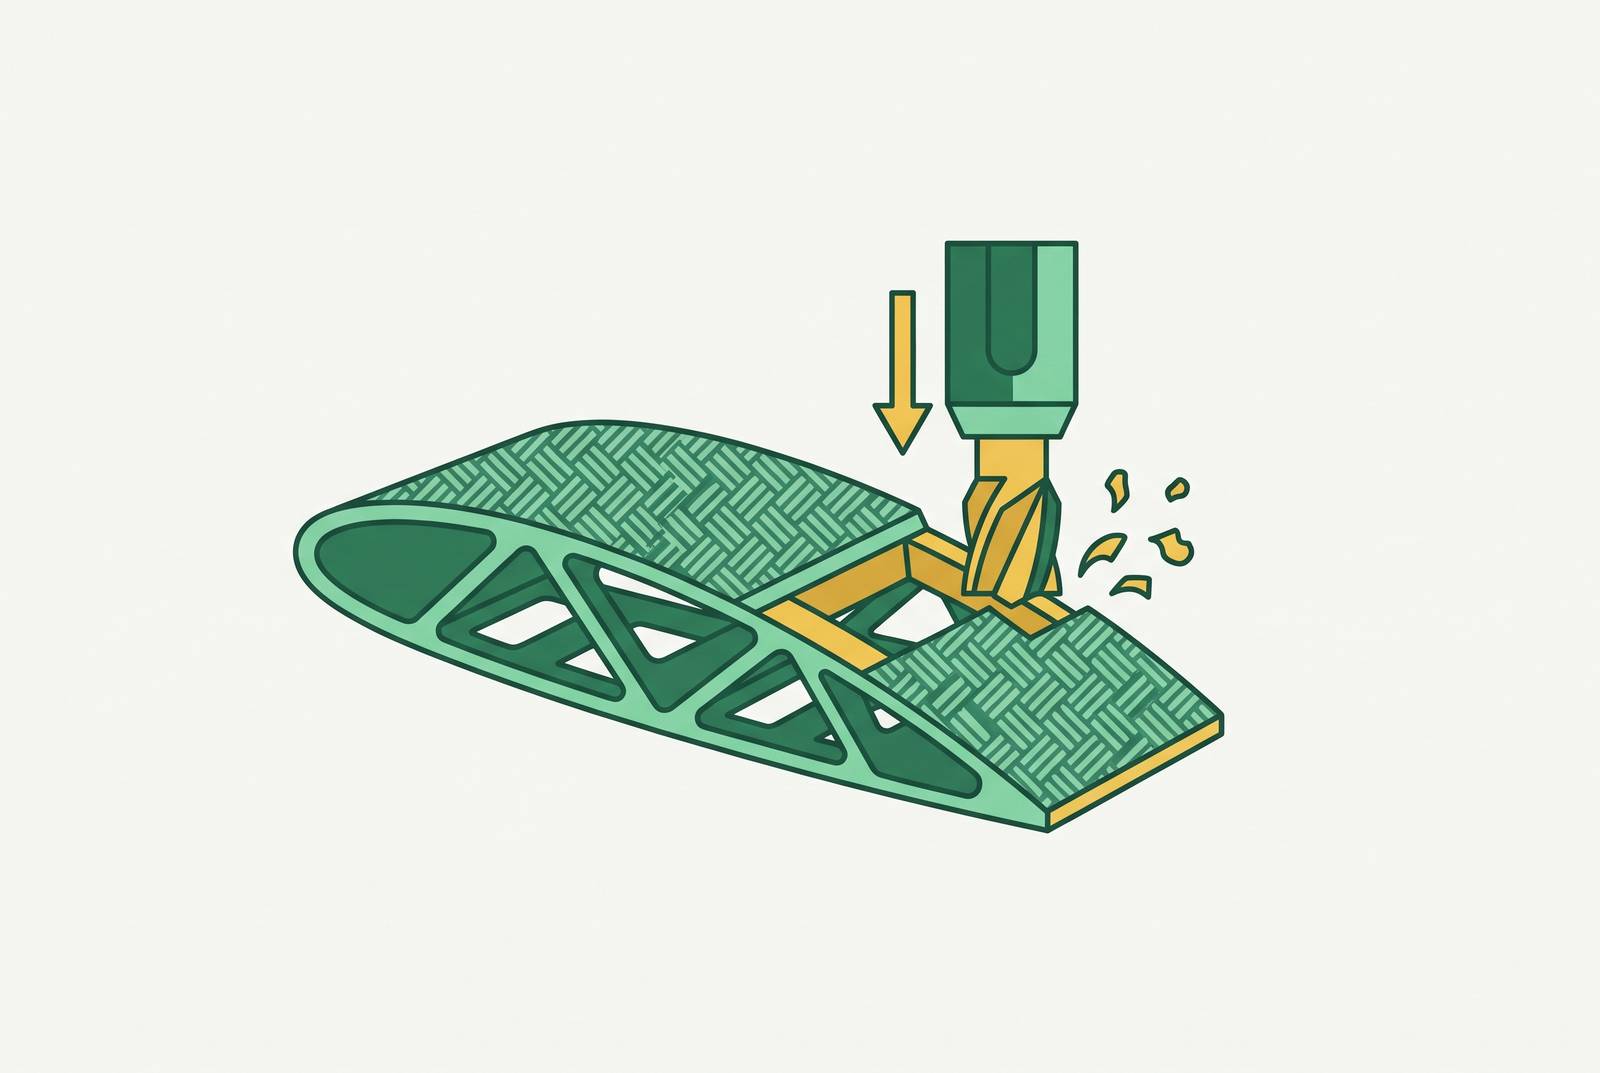
Tool geometry offers a real lever here. But geometry choices made way earlier, at the CAD stage, matter just as much. Thin walls, sharp internal corners, and hole patterns spaced too closely together all concentrate cutting force in ways that raise delamination probability before a machinist ever touches the part. Counterintuitively, cutting fast and decisively tends to beat a slow, hesitant pass. A tool that dwells or decelerates mid-cut generates more heat and more pushing force, and both of those push delamination risk higher, not lower. A low helix angle (10–15 degrees maximum) on milling tools keeps milling operations from pulling the material apart, and compressive helix cutters specifically designed for composite trimming address the same problem.
Heat management and the glass transition temperature boundary
The resin matrix holding those carbon fibers together is thermally sensitive in a way metal isn't. Machining-induced heat causes delamination, burr formation, and microstructural damage, and the risk climbs sharply once temperatures cross the glass transition temperature, or Tg, of the resin system. Tg is the real boundary here, not an arbitrary specification number.
That same study reveals a trade-off worth sitting with. Cryogenic machining, cutting to stay below Tg, improved performance overall but reduced residual intensity by about 7.14%, a consequence of Tg-based viscoelasticity in the resin Deformation Resistance Performance of Carbon Fiber-Reinforced Plastic Machined by Controlling Drilling Area Temperature below the Glass Transition Temperature. Thermal management, in other words, isn't a free lunch. Pushing the temperature down too aggressively causes a different property to give up ground somewhere else.
There's also a defect that doesn't announce itself visually: the heat-affected zone, or HAZ, is a ring of thermally degraded resin surrounding the cut that isn't always visible under normal inspection, yet it still compromises the local mechanical properties of the part. That's a structural concern sitting quietly apart from anything you'd catch by eye or by caliper.
Coolant strategy compounds the decision. Liquid coolant, standard practice in metal machining, raises contamination and delamination risk on CFRP in certain configurations, so dry cutting paired with high-volume air evacuation is often the preferred route, even though it limits how much heat actually leaves the cut zone. Knowing which regime applies to a given part, and why, isn't optional information for whoever's running the machine.
Features that keep a tool engaged in one spot for a long stretch, deep pockets, long slot runs, thick sections, are thermal risk zones by definition. Breaking those features into shorter passes, or redesigning the part so the tool doesn't dwell there as long, is a geometry decision that has to happen before the file ever reaches a machinist. Heat and delamination, described this way, still read as if they behave the same regardless of direction. They don't. Fiber orientation determines which way both of these failure modes actually propagate through the laminate. The glass transition temperature (Tg) is the controlling boundary, and keeping the drilling area below Tg is a documented technique for preserving deformation resistance.
Fiber orientation and anisotropy as a design variable, not just a material property
CFRP's anisotropy means stiffness, strength, and how the material fails all depend on the angle between the load and the fiber direction. Layup sequence is a design output, chosen ply by ply, rather than a default setting inherited from convention. It's a design output, chosen ply by ply. Each ply gets assigned a specific fiber orientation, and that assignment is what determines stiffness, strength, and failure behavior for that section of the part, a decision made well before any machining begins.
Machining interacts directly with that orientation. Cutting fibers at different angles relative to the tool path changes surface quality, changes which direction burrs form, and changes how likely the cut is to delaminate. A pocket milled parallel to a 0 degree ply behaves nothing like the same pocket cut across a 90 degree ply. A common failure mode occurs when composite parts get designed like sheet metal: shape decided first, material assignment bolted on second, manufacturability considered last, if at all. That sequence, treating composites design like sheet metal with shape first, material assignment second, and manufacturability last, ignores fiber tailorability entirely.
The structural stakes of ignoring orientation at a machined feature are concrete. Edge-loaded holes, cutouts placed near a load path, and trimmed edges all interact with whatever ply stack sits underneath them locally. Cutting fibers at different angles to the tool path produces different surface quality, burr direction, and delamination tendency, so a pocket machined parallel to a 0° ply behaves differently from one crossing 90° fibers. Waterjet and CNC cutting both damage the continuous fibers right at the cut edge, and that edge damage cuts tensile strength by 30 to 50% ScienceDirect 2025 review Industrial Monitor Direct. That penalty isn't uniform either, it's orientation-dependent, and it has to get built into the structural margin near any machined boundary rather than assumed away.
AFP's kinematics, process parameters, and the data gathered during layup all feed back continuously into design optimization. Fiber orientation at every machined feature, holes, pockets, trim lines, joint surfaces, needs to be called out explicitly on the drawing for anyone drawing up a structural CFRP part. Leaving it to whoever runs the fabrication floor to decide is how a good design turns into an inconsistent part.
Tolerance control across secondary machining operations
Near-net-shape layup and curing gets a CFRP part most of the way there, but not all the way. Secondary machining, turning, milling, and drilling performed after the cure cycle, is what actually delivers the required tolerances and produces the fitting and joining surfaces the assembly needs. On a structural aerospace part, that step isn't optional, and it isn't a formality either.
The tolerance challenge compounds because every constraint covered so far, tool wear, delamination, heat, fiber orientation, introduces its own slice of dimensional error independently. When they stack together on a single part, the error isn't additive, it's multiplicative. Five-axis CNC machining helps contain that by letting a shop hold a complex part in a single fixture through the whole operation, which cuts out setup-induced error that would otherwise appear every time the part gets unclamped and repositioned. For structural parts with compound curves and features on multiple faces, that single-fixture approach isn't a convenience. It often means the tolerance is held or not.
Hole tolerance deserves particular attention, because it's arguably the single most critical feature class on a structural CFRP part. Fastener holes for riveted or bolted joints carry both a diameter tolerance and a perpendicularity tolerance, and delamination forming at the entry or exit face violates both requirements at once. Surface finish matters just as much in places that don't look critical at first glance: bonded joints, seal interfaces, co-cured surfaces all carry their own roughness requirements, and dull tooling combined with thermal damage degrades that finish directly.
Given how many failure modes converge on a finished part, dimensional inspection by itself isn't enough to sign off on it. Visual inspection and non-destructive testing methods are both needed to confirm there's no delamination sitting hidden inside the laminate. Any tolerance called out on a drawing that's tighter than what the process can reliably hold, given known tool wear rates, the thermal regime in use, and the fixturing plan, needs to get flagged at the quoting stage. Waiting for that discovery until first-article inspection is the expensive way to find out.
Non-conventional machining methods that resolve conventional limits
Conventional CNC isn't the only tool in the box, and for certain features it isn't even the best one ScienceDirect 2025 review Industrial Monitor Direct. A 2025 review in the Journal of Mechanical Engineering catalogs several methods developed specifically to address CFRP's quirks: laser beam machining, electrical discharge machining (EDM), abrasive water jet machining (AWJM), and electrochemical discharge machining (ECDM).
AWJM looks especially promising for aerospace CFRP work because it generates no heat-affected zone and involves no tool contact with the part at all. Surface irregularities and dimensional instability are still documented problems with the process, so it isn't a universal fix. Laser machining carries its own trade-off. Millisecond-pulse lasers cause significant matrix vaporization, leave recast material behind, and can trigger interlaminar delamination and microcracking, dropping residual tensile strength to somewhere around 259.0 MPa in tested samples ScienceDirect. Femtosecond laser systems are being studied as a more precise alternative that might avoid some of that damage.
GE Aviation's water jet-guided laser system, confirmed by Composites World and known as MicroJet, offers a concrete benchmark for what a hybrid approach can deliver: drilling CFRP/CMC material in 2 minutes, against roughly 1 hour using conventional machining for the same feature. That's not an incremental gain; it's a different order of magnitude, and it shows where non-conventional methods earn their keep.
Choosing among these options comes down to matching the method to the feature. Conventional CNC remains the default choice for complex 3D geometry and tight tolerances on surfaces a tool can actually reach. AWJM suits 2D profiling work where any heat-affected zone is unacceptable. Laser and hybrid methods fit high-volume small-diameter holes cut into thin sections. No single method here erases every constraint discussed so far, each one just trades one failure mode for a different one, so the structural requirement of the specific feature should drive the choice, not whatever equipment happens to be sitting on the shop floor.
DFM principles for CFRP aerospace parts: geometry decisions that determine machinability before a tool is selected
A study out of SAAB Aerostructures makes the underlying point: manufacturability has to get considered during aircraft design itself if the resulting part is going to be cost-effective to actually build. Everything covered above points toward a short list of design-stage habits that keep a CFRP structural part machinable instead of merely drawable.
Fiber orientation belongs on the drawing at every machined feature, holes, pockets, trim lines, called out explicitly rather than left for a shop to infer. Thin walls and sharp internal corners in load-carrying sections concentrate cutting force and should get redesigned wherever possible, and hole patterns need spacing that avoids stacking closely spaced holes into a single ply region, since the ligament between them is a real structural and machining risk. Tight-tolerance features should sit away from part edges, where that 30 to 50% tensile strength penalty from fiber cutting is already eating into the margin ScienceDirect 2025 review Industrial Monitor Direct. Post-machining steps, sanding, fine-grit finishing, resin coating on bonded or sealing surfaces, belong in the process plan from the outset, not as a fallback when a part fails inspection. The resin system's Tg needs to appear on the drawing too, because the machinist setting thermal limits for that cut needs that number in hand, not a general assumption about epoxy behavior. Multi-material stack interfaces such as CFRP/titanium and CFRP/aluminum should be flagged explicitly in the BOM and drawing notes, since they require different cutting parameters mid-operation.
This only works if it happens before a purchase order gets cut. DFM feedback belongs in the quoting conversation, so that when a shop reviewing a part file spots a tolerance or a geometry the process can't reliably hold, that conversation happens before manufacturing starts, not after the first article comes back rejected. A structural CFRP assembly is rarely just CFRP anyway. It carries fasteners, inserts, bonded metal fittings, gaskets, surface treatments, and sourcing each of those from a separate vendor multiplies schedule risk and stacks tolerance error on top of tolerance error by the time everything reaches final assembly. Handling CFRP machining alongside the rest of what a structural aerospace assembly actually needes, CNC milling and turning, sheet metal, custom gaskets, tube bending, with DFM feedback built into quoting rather than bolted on afterward, is what keeps a design that looks right on screen from turning into a rejected first article on the shop floor. Core DFM principles derived from the constraint map.
Sources
- Machinability optimization of carbon fiber reinforced polymer composites for aviation manufacturing parts | Multidiscipline Modeling in Materials and Structures | Emerald Publishing
- A Review of Non-conventional Machining of Carbon Fibre Reinforced Plastic Composite
- Material performance, manufacturing methods, and engineering applications in aviation of carbon fiber reinforced polymers: A comprehensive review - ScienceDirect
- Aerospace Production: Overcoming Challenges in Composite Machining - Mobility Engineering Technology
- Deformation Resistance Performance of Carbon Fiber-Reinforced Plastic Machined by Controlling Drilling Area Temperature below the Glass Transition Temperature
- Laser machining of carbon fiber reinforced polymer (CFRP) – progress and challenges - ScienceDirect
- Design for Manufacturing of Composite Structures for Commercial Aircraft – The Development of a DFM Strategy at SAAB Aerostructures - ScienceDirect
- Carbon fibre for applications in aerospace: A review - ScienceDirect