Sheet Metal Bend Radius Rules for Aluminum vs. Steel Enclosures
Tight bend radii crack parts unless you match alloy, temper, and grain direction to the press brake.
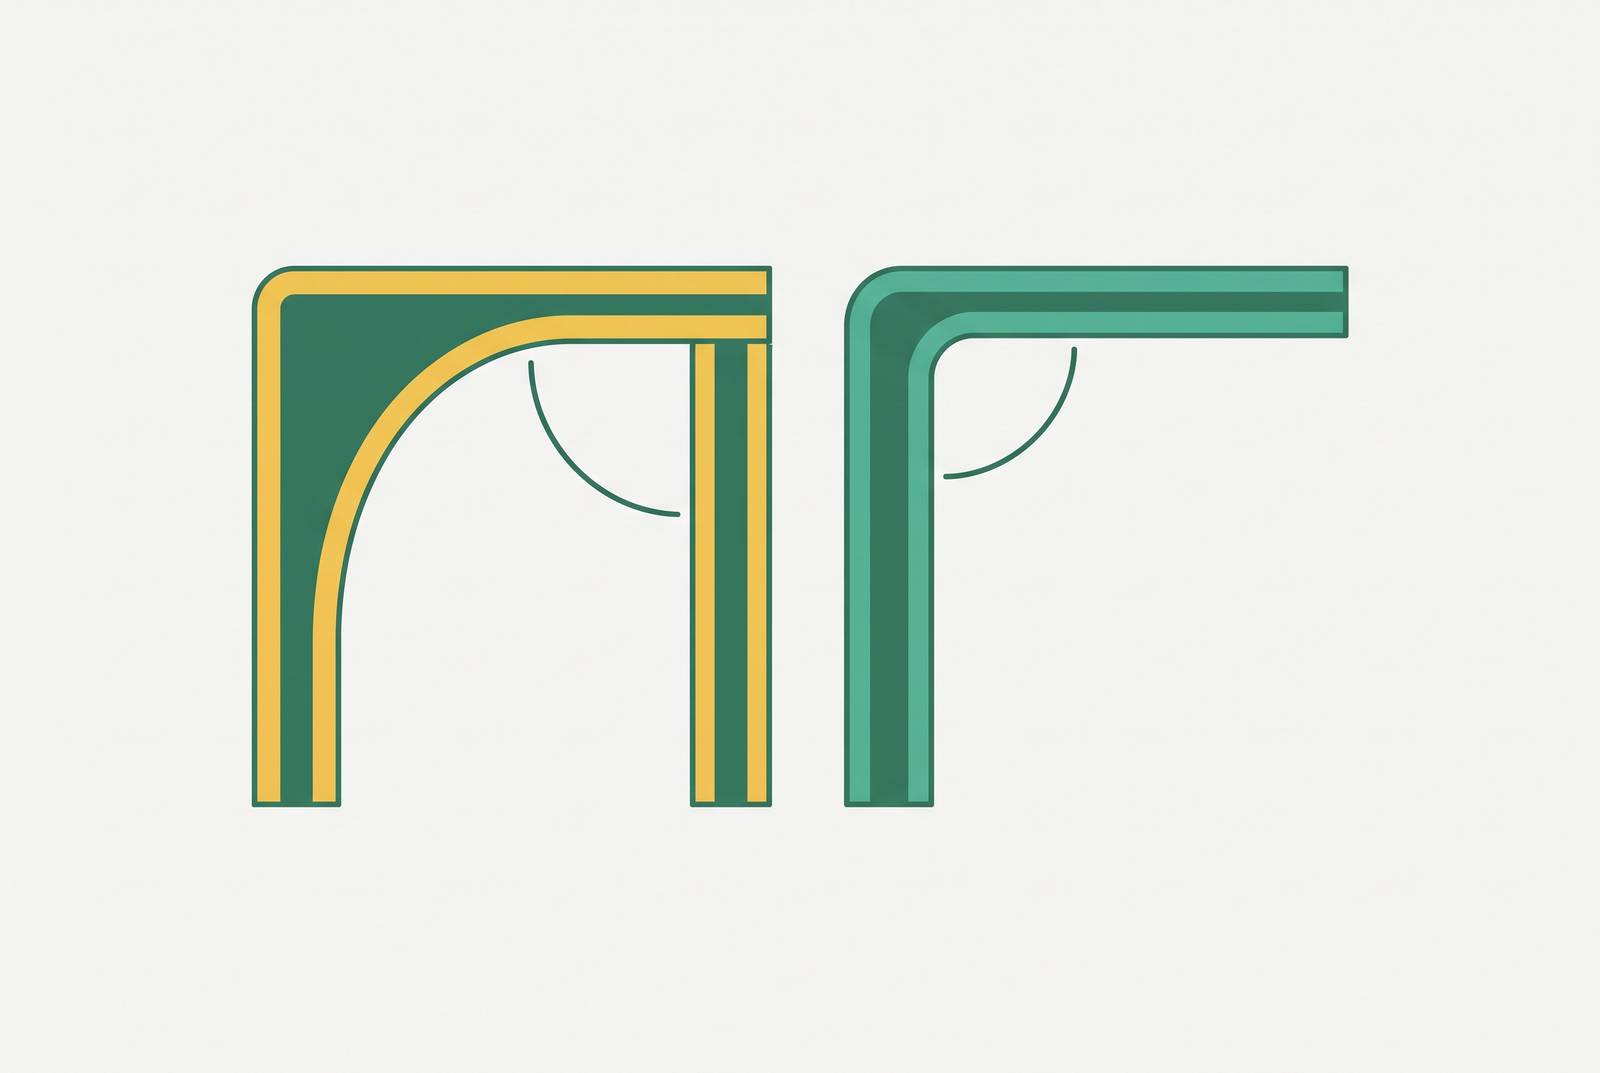
Bend radius on sheet metal isn't a cosmetic spec. It's the number that decides whether a part clears the press brake clean or cracks on the first article. Get the alloy, temper, and grain direction wrong at the design stage, and the shop either scraps parts or calls with a change order nobody budgeted for.
Aluminum: how the 5052-H32 versus 6061-T6 divide plays out at the press brake
5052-H32 is the workhorse of enclosure sheet metal, and for good reason. Most gauges take a minimum inside radius of 1T (one times material thickness). Push it further, and thin stock bent across the grain can hit 0.5T with the right tooling. That's tight, and it's why so many enclosure panels default to this alloy without a second thought.
6061-T6 behaves very differently. Minimum radius jumps to 3T to 6T, and the reason comes down to temper. T6 heat treatment gives the alloy high yield strength and pulls out a lot of the ductility that lets metal fold without tearing. The same properties that make 6061-T6 great for machined structural brackets work against it the moment it hits a V-die.
The numbers back this up. First-article data on 1.5 mm 6061-T6 brackets shows roughly 1 out of 3 parts cracking when the print calls out R1.5 (1x thickness). Bump that to R4.5 (3x thickness), and the cracking disappears across every orientation tested. The dimensional cost of that fix: under 0.3 mm change on a 40 mm flange. Most enclosure layouts swallow that without a redesign.
So what does this mean for a part that needs both machining and bending? 6061-T6 still makes sense for the machined zones, but the designer has to plan the bent flanges around that 3T to 6T floor from the start, not after the first article cracks. If a tight radius on 6061-T6 truly can't be avoided, local annealing of the bend zone before forming is the workaround, though it's a secondary operation. It adds cost and lead time, and that needs to show up on the quote, not surprise anyone at first article.
Aluminum runs about a third the density of steel, which is exactly why it's the default for weight-sensitive enclosures. But that weight savings only counts if the alloy choice doesn't force a heavier gauge to make up for lost bend ductility. Pick the alloy based on the tightest bend in the design first, then check whether the machined features still work in that alloy. Not the other way around.
Grain direction shifts aluminum bend radius requirements by one to two thickness increments
Rolled sheet metal has a grain, and that grain runs in the direction the mill rolled it. Bend across that grain (perpendicular to it), and the material tolerates a tighter radius, somewhere in the range of 20 to 30% tighter than bending parallel to it, as Fabcon's sheet metal design guidelines state.
For 5052-H32, that difference is the gap between 0.5T and 1T. Bend thin stock across the grain, and 0.5T is achievable. Bend the same material parallel to the grain, and the requirement doubles to 1T. One orientation change, double the radius requirement.
6061-T6 sees the same effect, just stacked on top of an already steep baseline. Bending parallel to grain adds another 1 to 2 thickness increments on top of the 3T to 6T minimum.
A box enclosure has four sides, and grain direction only runs one way through the blank, so not every bend on that box can run perpendicular to the rolling direction at the same time. A box enclosure has four sides, and grain direction only runs one way through the blank. Not every bend on that box can run perpendicular to the rolling direction at the same time. The fix is to identify whichever bend is tightest, orient the blank so that specific bend crosses the grain, and accept that the other bends on the same part might need a slightly relaxed radius to compensate.
Drawings rarely call out grain direction explicitly. Left unspecified, the shop infers it from how the blank gets nested on the sheet, which means two runs of the same part can come out with two different grain orientations relative to the bend. That's a common, quiet source of inconsistent first-article results on tight-radius 5052-H32 parts, and it's avoidable with one callout on the drawing.
Tooling surface finish matters here too. Getting to 0.5T on 5052-H32 requires polished tooling that cuts friction at the bend. Standard tooling, even with correct grain orientation, may not get there.
Mild steel and 304 stainless: where the two materials diverge on radius, force, and springback
Mild steel, whether 1018 or A1008 cold-rolled, is the most forgiving material on this list. Minimum bend radius runs 0.5T to 1T, and Machinery's Handbook (31st Edition) assigns it a K value of 1.5, low and predictable.
304 stainless in the annealed state needs 1T to 2T minimum, higher than mild steel despite both being iron-based alloys. As stainless bends, the bend zone itself work hardens, getting harder and raising local yield strength right where the material needs to flex most.
Force requirements track a similar pattern. Aluminum needs roughly half the tonnage steel does, while stainless needs about one and a half times steel's tonnage. For a shop running a fixed press brake, that difference in force sets a hard ceiling on how thick a stainless part can get before the machine simply can't bend it.
Springback tells its own story. Mild steel (Q235 grade) springs back only 1 to 2 degrees after the punch releases. 304 and 316 stainless can spring back 3 to 5 degrees under identical tooling. That gap matters a lot when a panel has to nest precisely against another part.
Chaoero's shop data shows how this plays out in practice: a stainless part targeting a 90-degree bend rebounded to about 95 degrees on the first trial. The fix was overbending to 85 degrees using appropriate tooling selected for the overbend. After two to three rounds of tuning, the angle settled at 90 degrees, plus or minus half a degree, showing the process is iterative. It's an iterative process that costs setup time. It's iterative, and it costs setup time.
Anything tighter than plus or minus 1 degree on a stainless bend means the shop needs to run that qualification cycle, and that's a real cost to plan for at quoting, not a mistake to blame on the floor.
Advanced high-strength steel, if it shows up in structural enclosure work, needs 1.5 to 3 times thickness minimum radius. Force a standard 1T radius onto AHSS, and it cracks in roughly 90% of applications.
So the material call comes down to priority. Mild steel wins when cost and formability matter most. Stainless earns its place when corrosion resistance or finish appearance is non-negotiable, and the designer accepts the springback tuning that comes with it.
Air bending and V-die selection in shop-floor radius
Air bending runs most CNC press brake work today. The punch tip touches the sheet at one point, and the two edges of the V-die touch it at two more. That's it, three contact points, and the resulting radius floats based on the die opening width rather than the punch's own radius.
There's a rough rule that ties material to that radius: the inside bend radius comes out to roughly a fixed percentage of the die opening. Figures from jstmt.com put mild steel at about 16% and aluminum at 12 to 15%, while stainless runs 20 to 22%. That means the same die opening produces different radii depending on what's loaded in the brake.
Anyone specifying by the numbers alone runs into trouble here. A drawing calling out 0.030 in. radius on stainless and 0.030 in. on aluminum looks identical on paper, but the shop sets up completely different tooling to hit that same number on each material.
Approved Sheet Metal treats 0.030 in. as something close to an industry standard, a radius that lines up with common tooling and works across most materials and thicknesses up to 0.125 in. The exception is 6061-T6, which often needs something bigger to avoid cracking, a fact that circles right back to the alloy discussion above.
There's a practical cost lever hiding in all this: design every bend on a part to the same radius, and the shop never swaps tooling mid-run. That single decision, made at the CAD stage, saves setup time on every part that comes off the line.
K-factor rounds out the picture. It ranges from 0.3 to 0.5 depending on material and radius, aluminum usually runs near 0.4, and steel runs closer to 0.45. This number controls how much material the bend itself consumes, and it feeds directly into the bend allowance formula. Get the K-factor wrong, and every flange length on the flat pattern comes out wrong too.
SolidWorks ships with a default inside bend radius of 0.100 in. unless someone changes it. Standard tooling can't produce that radius, which means leaving the default in place triggers custom tooling charges nobody asked for. Set the radius on purpose, every time.
The enclosure-specific DFM rules that depend directly on bend radius
Flange length has a floor, and that floor is set by radius. The minimum is roughly 2t plus the inside radius, enough to span the V-die opening, though the practical shop rule of thumb runs closer to 4T plus the bend radius. Flanges shorter than that form inconsistently, or need tooling nobody wants to source for one part.
Hole and slot placement near a bend follows the same logic. Holes need to be at least 2.5t plus the radius away from the bend line, or the forming process distorts them. EPOC CRAFTER's shop data gives a concrete case: a 3 mm hole placed just 1 mm from a bend line on 1.5 mm 5052-H32 distorted during forming and added 15 to 20% to the per-part cost on a 200-piece run. That's a real number attached to a small design oversight.
The radius requirement and the flange length requirement compound each other. Because 6061-T6 needs 3T to 6T radius, its minimum flange length runs substantially longer than an equivalent 5052-H32 panel at the same thickness. That's a layout constraint, and it belongs in the design phase, not discovered during review.
EPOC CRAFTER's radius callouts give a clean split: R at least 1x thickness for 5052-H32, 304 stainless, and 1018 cold-rolled steel, and R at least 3x thickness for 6061-T6 and 7075-T6. Grain direction affects these minimums, and bending parallel to the grain rather than across it generally requires additional radius margin.
Tolerance standards make stainless springback concrete. ISO 2768-1:1989, medium class, sets linear tolerances between plus or minus 0.1 mm and 0.8 mm and angular tolerances between plus or minus 5 arcminutes and 1 degree, depending on dimension. Stainless springback of 3 to 5 degrees simply doesn't fit inside the tight end of that range without active overbend compensation built into the program.
The single strongest lever available in this entire process is picking one radius for the whole enclosure and sticking to it. No tooling changes mid-run, consistent flat-pattern math, and no risk that one bend is dialed in while another sits at the edge of what the tooling can hold. When a design genuinely needs something nonstandard, a very tight bend on thick stock, or mixed alloys in one assembly, that needs to get flagged at quoting. Waiting for the shop to find it at setup costs more than the flag ever would.
Choosing between aluminum and steel for an enclosure when bend radius constraints are part of the decision
For weight-critical enclosures with moderate geometry and tight flanges, 5052-H32 remains the default, and it earns that spot honestly: 1T radius, strong formability, solid corrosion resistance.
Parts that need machined features alongside bent flanges point toward 6061-T6, but only if the designer plans for that 3T to 6T radius on every single bend up front. If the flange geometry can't fit that requirement, the better move is falling back to 5052-H32 or splitting the design into separate machined and formed parts.
Cost-sensitive work that leans on formability points to mild steel. At 0.5T to 1T minimum radius and a K value of 1.5 per Machinery's Handbook, it's about as forgiving as sheet metal gets, and it designs cleanly to standard tooling without much thought.
Where corrosion resistance or surface cleanliness for food or medical use is non-negotiable, 304 stainless earns its spot at 1T to 2T minimum radius. The tradeoff is accepting the springback tuning and tighter angular tolerance risk that comes bundled with the material.
Thick-gauge parts add another variable: force. Aluminum needs about half the tonnage of steel, stainless needs about one and a half times steel's tonnage, and at higher thicknesses, the press brake's available tonnage can become a constraint that shapes the material choice.
Rack-mount and industrial enclosures often mix materials outright, aluminum panels next to steel brackets next to stainless hardware, and each of those materials carries its own radius rule. Managing that mix through a single point of visibility at quoting, someone looking at the full bill of materials at once, keeps parts designed by different engineers from arriving at the shop with radius callouts that don't agree with each other.
That's really what a DFM review at quoting is for. Catching a 6061-T6 panel called out at 1T before it's cut is worth more than any fix applied after the fact. The dimensional cost of correcting R1.5 to R4.5 on a 40 mm flange comes in under 0.3 mm, comfortably inside enclosure assembly tolerances. A cracked first article costs a lot more than 0.3 mm ever will.